 Tiếng
Việt
 Tiếng
Anh
 Tiếng
Nhật


 Tiếng Anh


Front end trim molding machine
Application of motorbike front bumper molding machine.
The motorcycle front cover trim molding machine is one of CNC-VINA's specialized and automatic presses for the auto and motorbike industry. Along with servo press products, frame number engraving machines, machine numbers, brake oil pumps... this is a product that we have commercially produced and supplied to Vietnamese, Japanese, and Korean customers.
The automatic motorbike mask pressing machine helps improve accuracy, productivity and automation in the automobile and motorbike assembly industry.
Customers who need automatic machines please contact:
VIETNAM CNC & TECHNOLOGY APPLICATION JOINT STOCK COMPANY
Hotline: +84.916 63 9355 / +84.915 74 4664
Email: Sales01@cncvina.com.vn / Sales03@cncvina.com.vn
Product description

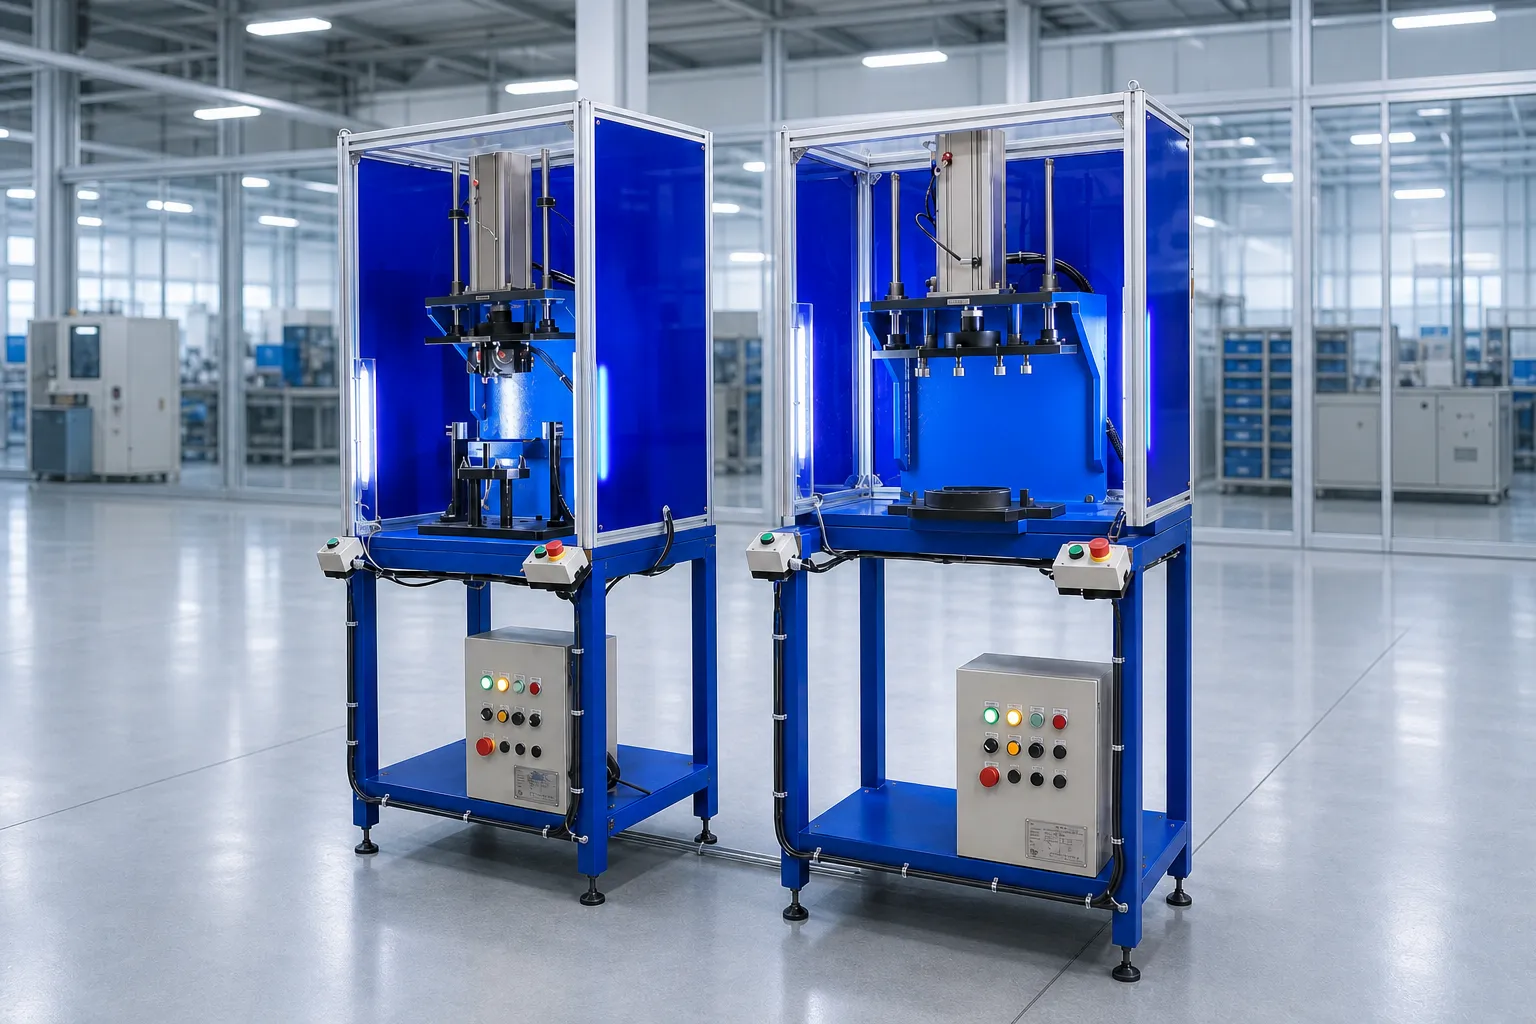
Front end trim molding machine is a specialized piece of equipment in the supporting machinery for the automotive and motorcycle manufacturing industry, designed for assembling plastic components around the front section of motorcycles. For certain motorcycle models from Honda, Yamaha, and Piaggio, the front head cover or front mask is fitted with an outer trim to complete the appearance and enhance the overall aesthetics of the product. Installing the trim requires the component to be correctly positioned and pressed along the appropriate profile to achieve consistent results after assembly. The Front Head Cover Edge Pressing Machine is developed to support this process, reducing manual operations and facilitating continuous production. The machine can be operated automatically or manually, depending on the requirements of the production line and the actual manufacturing process. With a configuration tailored to each product model, the machine can accommodate different requirements regarding pressing positions, component shapes, and operating methods. CNC VINA specializes in researching, designing, and manufacturing Front Head Cover Edge Pressing Machines based on actual product requirements, with configurations developed to suit each customer's assembly process and factory conditions.
Technical specifications of the Front end trim molding machine
| Machine dimensions | W960 x D900 x H1680 mm |
| Total power | 100 KW |
| Power supply | AC 380V, 3-phase, 50/60Hz |
| Control voltage | AC 220V, 24VDC |
| Number of operators | 1 operator |
| Weight | 90 kg |
Structure and operating principle of the Front end trim molding machine
The front head cover edge pressing machine features a simple and compact structure, equipped with a dedicated fixture and a pneumatic cylinder pressing mechanism designed to suit the shape of each product. The operating process follows the sequence of positioning – pressing – pressure holding – releasing, allowing the edge pressing process to be carried out quickly, consistently, and conveniently for operators.
Structure of the front head cover edge pressing machine
The Front Head Cover Edge Pressing Machine is designed with a simple, compact, and stable structure, making it suitable for installation in assembly areas within the factory. The machine consists mainly of a machine frame, product positioning fixture, pneumatic cylinder pressing mechanism, and control system. These components are arranged appropriately to facilitate quick product loading, pressing, and unloading.
Machine frame: The machine frame supports the entire system and provides structural stability during operation. Its structure is designed according to the product dimensions and actual installation space, allowing the machine to operate reliably in continuous production environments.
Product positioning fixture: This is an important component, specially designed by CNC VINA for each type of front head cover or motorcycle front mask. The fixture accurately positions the product and securely holds the component in place during the pressing process. Depending on the shape and requirements of each product, the fixture can be equipped with suitable support points, locating pins, or holding mechanisms to minimize product movement when pressing force is applied.
Pressing mechanism: The pressing mechanism uses a pneumatic cylinder to generate the force required to press the edge of the component. The cylinder is positioned according to the required pressing direction and location of the product. When receiving a signal from the control system, the cylinder moves along the preset stroke, bringing the pressing mechanism into contact with the component and carrying out the pressing process.
In addition, the control system allows the operator to activate and control the machine's operating cycle. The pressing time can be set using an external timer, allowing the pressure-holding duration to be adjusted according to the specific product and process requirements.

Motorcycle masks before and after being pressed automatically on a press designed and manufactured by CNC VINA
Operating Principle of the front end trim molding machine
The operating process of the front head cover edge pressing machine is designed to be simple, reducing the number of manual operations required and ensuring that each pressing step is carried out in a consistent sequence.
Step 1: Place the product into the fixture
First, the operator places the front head cover or motorcycle front mask into the fixture. The product is positioned according to the specified orientation and location so that the locating points on the fixture properly contact the component. Accurate positioning from the beginning ensures that the edge to be pressed is correctly aligned with the pressing mechanism, minimizing deviations during the operating cycle.
Step 2: Activate the pressing cycle
After checking that the product is correctly positioned, the operator activates the machine using the control button. The control system receives the signal and starts the pressing cycle. Depending on the machine configuration, it can be operated directly by the operator or integrated with an automatic mode within the production line.
Step 3: The pneumatic cylinder performs the pressing operation
When the cycle is activated, the pneumatic cylinder moves downward along the preset stroke. The pressing mechanism applies force to the cover edge, bringing the component into the required position. The pressing force is transmitted through the pressing mechanism to the area being processed. Since the fixture securely holds the product in place, the pressing process can be carried out consistently while minimizing product movement during operation.
Step 4: Hold the pressure for the preset duration
Once the pressing mechanism reaches the limit position, the system maintains the pressing state for the preset duration. This time can be adjusted using an external timer according to the characteristics of the product and the process requirements. Controlling the pressing time helps maintain consistency between operating cycles and eliminates the need for operators to manually estimate the required pressing duration.
Step 5: The pressing mechanism returns to its initial position
When the pressing time is completed, the pneumatic cylinder returns to its initial position. The pressing mechanism moves away from the product, creating sufficient clearance for the operator to remove the finished component from the fixture.
Step 6: Remove the product and start a new cycle
The operator removes the finished product from the fixture, performs a quick inspection, and places the next product into the positioning area. The pressing cycle is then repeated.
With this operating method, the entire process of product loading – positioning – pressing – pressure holding – releasing – product unloading follows a clear sequence, making the machine easy to operate while maintaining stable productivity during production.
Since each type of front head cover or motorcycle front mask may have different shapes and pressing positions, the fixture and pressing mechanism are designed by CNC VINA based on the actual product. The locating positions, support points, and pressing direction can be calculated and configured according to the requirements of each component. In addition, the pressing time can be adjusted to suit the product characteristics and specific manufacturing process. With this level of customization, the machine can be developed for different products and adapted to various requirements of motorcycle assembly lines.
Key features
The front head cover edge pressing machine features a compact structure, stable operation, and simple operation, making it suitable for various motorcycle assembly lines. The fixture and pressing mechanism are designed according to each product, allowing the edge pressing process to be carried out accurately, quickly, and conveniently for operators.
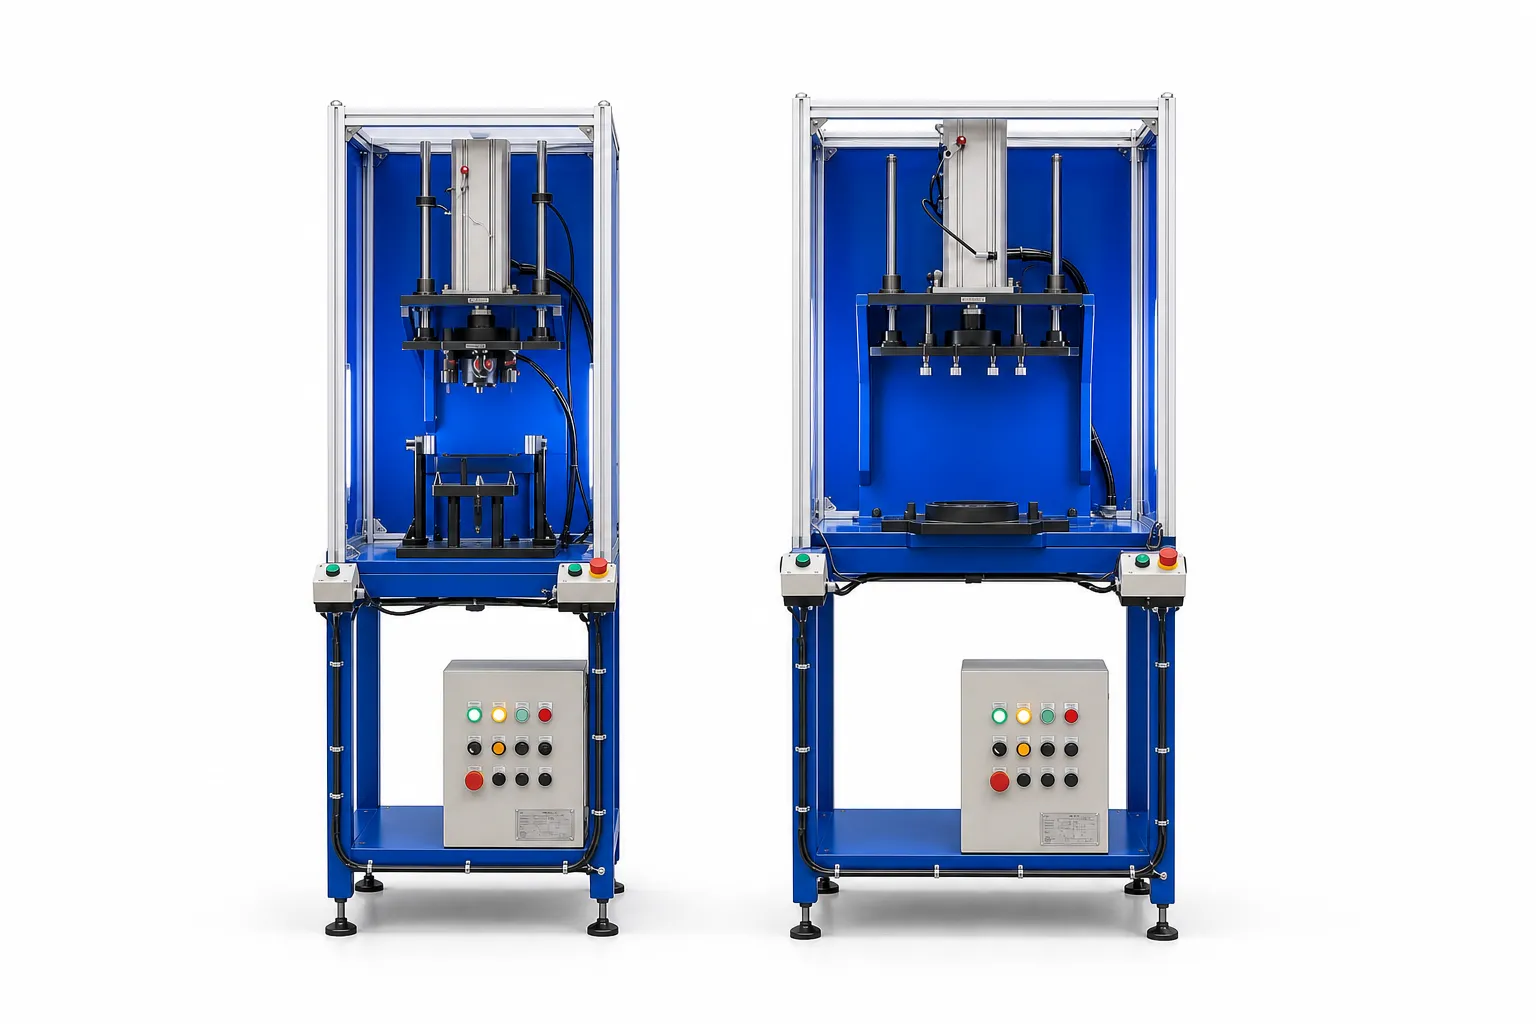
- The machine is arranged in a vertical frame structure, with the functional assemblies concentrated within a relatively compact space. The main components include the machine frame, product fixture, pressing assembly, and control system, providing the necessary functions for the pressing process without requiring an overly complex system. This structure also makes it convenient to inspect the machine components during operation. When cleaning, adjustment, or maintenance is required, operators can easily access the different assemblies.
- Each type of front head cover or motorcycle front mask has a different shape, so the fixture is designed based on the actual component to be pressed. Support points and locating positions are arranged to ensure that the product is correctly positioned before the pressing mechanism operates. Once the product is placed in the fixture, the component remains relatively stable throughout the pressing process. The edge to be pressed is positioned directly within the working area of the pressing mechanism, minimizing misalignment caused by incorrect product positioning.
- The machine's pressing assembly uses a pneumatic cylinder to generate the pressing movement. When the machine receives an operating signal, the cylinder moves in the designed direction and brings the pressing head down to the required position on the product. The cylinder stroke is limited according to the requirements of each pressing operation. Once the pressing position is reached, the mechanism maintains the pressure for the preset duration before returning to its initial position. This operating method allows each pressing cycle to follow the same sequence rather than relying entirely on manual operator actions.
- Depending on the intended application, the machine can be configured for automatic or manual operation. In automatic mode, after the product is placed into the fixture, the operator activates the cycle and the machine performs the pressing, pressure-holding, and releasing operations in sequence. Once the cycle is completed, the operator removes the finished product and loads the next component into the machine. In manual mode, the operator can control the machine operations directly. This configuration is convenient during trial runs, fixture inspections, product adjustments, or when the machine is used in processes that do not yet require full automation.
- With the pressing process carried out according to a fixed sequence, the machine allows operators to maintain relatively consistent operations from one product to another. Incorporating the pressing force and pressing time into the machine mechanism also reduces operations that would otherwise have to be performed manually. When combined with a feeding system or subsequent assembly processes, the machine can be arranged as a workstation within a production line, making it suitable for production processes requiring continuous and repetitive pressing operations.
- The preset pressing time eliminates the need for operators to manually determine the pressing duration for each product. Once the cycle is completed, the pressing mechanism automatically returns to its initial position and is ready for the next pressing cycle. This configuration is suitable for production processes involving large quantities of products and repetitive operations throughout the production shift.
The Front end trim molding machine is a suitable solution for businesses looking to improve the assembly process of motorcycle front plastic components. The equipment transfers part of the pressing operation from manual handling to a machine-based mechanism, helping to achieve greater consistency throughout the process. Depending on the product, the system can be configured with a suitable fixture and pressing mechanism to meet the actual requirements of the operation. The machine can also be installed as a standalone workstation or integrated with other equipment in an assembly line. With experience in designing automation equipment for the automotive and motorcycle industry, CNC VINA can develop the machine based on product samples, technical drawings, and the customer's production requirements. The design solution is developed according to the component characteristics, required production volume, and available factory space.
VIETNAM CNC & TECHNOLOGY APPLICATION JOINT STOCK COMPANY
Factory: Song Cung Industrial Site, Dong Thap Commune, Dan Phuong District, City. Hanoi Vietnam
Phone: +84.916 63 9355 / +84.915 74 4664
Website: https://cncvina.com.vn; https://cncvina.net; https://cncviname.com.vn
Email: Sales01@cncvina.com.vn | Sales03@cncvina.com.vn


